What Are the 2026 Top Aluminium Melting Furnace Types?
Choosing the right aluminium melting furnace in 2026 requires more than comparing purchase prices. Foundries now examine energy consumption, melting speed, alloy cleanliness, emissions, maintenance, and production flexibility. The most discussed options include gas-fired reverberatory furnaces, electric resistance furnaces, induction furnaces, crucible furnaces, and rotary systems. Each design serves a different operating reality.
A large automotive foundry may prefer a reverberatory furnace because it handles high volumes and continuous charging. A smaller job shop may value an induction furnace for rapid heating, precise temperature control, and reduced material contact. Electric resistance models can provide stable heat for controlled batches, while crucible furnaces remain practical for lower output and varied alloy work. Rotary furnaces can recover metal efficiently from certain scrap streams, although their performance depends heavily on charge preparation and operator skill.
The “top” aluminium melting furnace is not automatically the newest or most expensive model. That assumption is too simple. Experienced operators often notice details that brochures overlook, such as dross buildup near the door, uneven heat around the crucible, or delays during alloy changes. These observations matter. Reliable selection should combine supplier data, independent testing, real production records, and a clear assessment of workplace conditions. Fuel availability, electrical capacity, ventilation, refractory life, and local environmental requirements can change the final decision. Some performance figures may also vary between laboratory tests and busy factory floors. That uncertainty deserves attention. This guide compares the leading furnace types for 2026, explains their practical strengths and limitations, and identifies where each aluminium melting furnace can deliver dependable value.
How Aluminium Melting Furnaces Are Classified in 2026
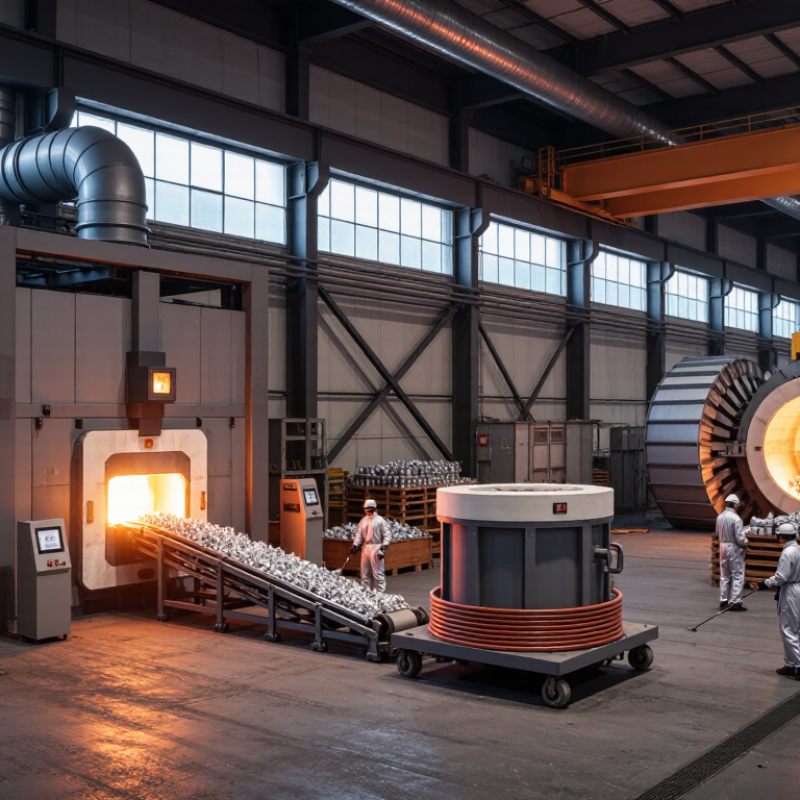
In 2026, aluminium melting furnaces are classified by heat source, chamber design, metal handling, and production scale. This method is more practical than naming one furnace as universally best.
Fuel-fired furnaces use approved combustion fuels, while electric models use resistance or induction heating. Heat source affects energy cost, installation, emissions control, and temperature response. In a foundry, these differences appear quickly. Slow heating can delay casting, while uneven heating may increase oxide formation.
Crucible furnaces melt aluminium inside a removable or fixed vessel. They suit small batches, frequent alloy changes, and flexible workshop production.
Reverberatory furnaces heat the charge through a roof and hearth. They support larger volumes and longer production cycles.
Rotary furnaces use a rotating chamber to improve contact between the charge and heated surfaces. They can handle varied feedstock, but lining wear and dross control need regular inspection.
Induction furnaces generate heat inside the metal through electromagnetic fields. They offer rapid response, although electrical capacity and coil maintenance require careful planning.
Another classification considers furnace movement. Fixed furnaces discharge through a tap hole, while tilting furnaces rotate for controlled pouring. Holding furnaces keep molten aluminium near the casting line.
Systems also differ in control level, from manual burners to sensor-based temperature management. Operating temperatures often stay near 700 to 760°C, depending on alloy and process.
Higher heat is not automatically better. It may increase oxidation and hydrogen absorption.
Capacity labels can also mislead when they ignore melt rate, door openings, and recovery time. That mismatch is easy to miss during equipment selection.
Gas-Fired Reverberatory Furnaces for High-Volume Aluminium Melting
What Are the 2026 Top Aluminium Melting Furnace Types?
Gas-fired reverberatory furnaces remain a practical choice for high-volume aluminium melting. They suit foundries that need steady output, large charge capacity, and flexible batch handling. Burners heat the furnace roof and walls, while reflected heat melts aluminium across a broad hearth. This indirect heating method reduces direct flame contact with the metal. It can also support cleaner melt quality when the furnace atmosphere is carefully controlled. Good refractory design matters.
In daily operation, operators often preheat the hearth before adding sorted aluminium charge. This reduces thermal shock and helps prevent localised cold spots. Accurate temperature sensors guide burner adjustment and tapping decisions. Recuperative or regenerative systems can lower fuel demand by recovering heat from exhaust gases. However, performance depends on burner tuning, door sealing, refractory condition, and charge preparation. Small leaks waste energy.
The main weakness is slower response than some compact furnace designs. A large chamber may also increase holding losses during production delays. Operators should record melt temperature, fuel use, dross formation, and furnace pressure. These records reveal problems that visual checks may miss. Regular inspection of burner flames and refractory wear improves reliability. No furnace is perfect. A gas-fired reverberatory furnace performs best when capacity, fuel efficiency, emissions control, and maintenance planning are evaluated together.
What Are the 2026 Top Aluminium Melting Furnace Types? - Gas-Fired Reverberatory Furnaces for High-Volume Aluminium Melting
| Furnace Type | Typical Usable Capacity | Typical Melt Rate | Typical Operating Temperature | Main Fuel Options | Key Advantages | Best-Fit Application |
|---|---|---|---|---|---|---|
| Fixed-Hearth Direct-Fired Reverberatory Furnace | 2–50 tonnes | 1–15 tonnes/hour | 700–780°C metal temperature | Natural gas, LPG, renewable gas blends | Simple construction, high charging flexibility, suitable for continuous production | High-volume melting of ingot, foundry returns, and clean aluminium scrap |
| Tilting Reverberatory Furnace | 2–30 tonnes | 1–12 tonnes/hour | 700–780°C metal temperature | Natural gas, LPG | Fast drainage, reduced residual metal, easier alloy changeover and cleaning | Multi-alloy foundries requiring flexible batch operation |
| Sidewell Reverberatory Furnace | 5–80 tonnes | 3–30 tonnes/hour | 680–760°C metal temperature | Natural gas, LPG, low-carbon gas blends | Separates melting from pumping or holding; supports controlled metal transfer | Large die-casting and continuous casting operations |
| Dry-Hearth Charging Reverberatory Furnace | 5–60 tonnes | 2–25 tonnes/hour | 700–780°C metal temperature | Natural gas, LPG | Preheats the charge, improves throughput, and can reduce direct flame contact with molten metal | Operations using substantial quantities of solid ingot or clean scrap |
| Twin-Chamber Reverberatory Furnace | 5–100 tonnes | 3–40 tonnes/hour | 680–780°C metal temperature | Natural gas, LPG, renewable gas blends | Separate charging and melting zones can improve scrap handling and process continuity | Large recycling plants and high-throughput secondary aluminium production |
| Regenerative-Burner Reverberatory Furnace | 10–100+ tonnes | 5–40+ tonnes/hour | 700–780°C metal temperature | Natural gas, LPG, renewable gas blends | Recovers heat from exhaust gas, supports high firing rates, and can reduce fuel use compared with conventional burners | Energy-intensive plants with long operating hours and high annual output |
| Low-NOx Gas-Fired Reverberatory Furnace | 5–100 tonnes | 3–40 tonnes/hour | 680–780°C metal temperature | Natural gas, LPG | Staged combustion or flue-gas recirculation can lower nitrogen oxide formation | Plants operating under strict air-emission requirements |
Electric Induction Furnaces for Precise and Flexible Melting
What Are the 2026 Top Aluminium Melting Furnace Types?
Electric induction furnaces are gaining attention for precise and flexible aluminium melting. They heat the metal directly through electromagnetic fields. This reduces flame exposure and supports cleaner, more controlled workshops. Operators can adjust power quickly when alloy recipes change. That matters for foundries producing small batches or several grades daily. Temperature stability also helps reduce oxidation, dross, and avoidable rework. The U.S. Department of Energy identifies induction heating as an efficient industrial method because energy transfers directly into the charge. However, efficiency depends on coil design, furnace loading, insulation, and operator practice.
The International Aluminium Institute reports that recycled aluminium requires about 5% of the energy used for primary aluminium production. Induction furnaces fit this circular model well, especially when melting clean, sorted scrap. They can also support digital temperature tracking and automatic power control. Still, induction is not automatically green. Electricity sources, poor loading, and repeated holding cycles can weaken its environmental value. I may be too optimistic here. Every installation needs measured energy data.
Tips: Check the furnace’s useful melting rate, not only its electrical rating. Record kWh per tonne, melt loss, holding time, and cleaning frequency. Keep charge materials dry and consistent. A compact induction furnace may look ideal, yet oversized capacity can increase standby losses. The best 2026 choice balances precision, flexibility, maintenance access, and verified operating data.
Electric Resistance and Crucible Furnaces for Small-Batch Production
What Are the 2026 Top Aluminium Melting Furnace Types?
Electric Resistance and Crucible Furnaces for Small-Batch Production
For small-batch aluminium production, electric resistance and crucible furnaces remain practical choices in 2026. Electric resistance furnaces heat the chamber evenly through controlled heating elements. They suit workshops producing repeated batches with stable alloy requirements. Digital temperature control can reduce overheating and unnecessary holding time. Clean operation matters near casting benches.
Crucible furnaces offer a simpler setup. Operators can melt smaller charges, change alloys quickly, and inspect the metal directly. They are useful for repair work, prototypes, laboratory casting, and short production runs. However, manual handling can increase heat loss and temperature variation. That weakness is easy to underestimate.
The International Aluminium Institute reported global primary aluminium production near 70 million tonnes in 2023. The scale highlights aluminium’s energy demands, even though small foundries operate differently. The International Energy Agency identifies aluminium as using about 4% of global electricity consumption. Therefore, furnace selection should consider standby power, insulation, batch size, and melt-loss control.
Published efficiency figures need caution. Real performance changes with charge geometry, door opening, crucible condition, and operator habits. An electric resistance furnace may deliver better repeatability, while a crucible furnace may reduce investment risk. Neither option is automatically superior. Measure actual kWh per kilogram, melt time, dross generation, and temperature recovery before purchasing. Small details matter.
Comparing Furnace Types by Efficiency, Capacity, Emissions, and Control
What Are the 2026 Top Aluminium Melting Furnace Types?
Choosing a 2026 aluminium melting furnace starts with the charge, not the brochure. Gas-fired reverberatory furnaces suit large batches and mixed ingot. Rotary furnaces tolerate oily, painted, or heavily oxidized scrap, but slag handling can reduce effective yield. Coreless induction furnaces deliver fast response, clean temperature control, and strong repeatability. They often fit smaller or medium batch cells, especially where electricity is reliable. No furnace wins every test.
The International Aluminium Institute reported in 2024 that recycled aluminium requires up to 95% less energy than primary aluminium. That figure describes the material route, not furnace efficiency, and this distinction matters.
The U.S. Department of Energy reported in 2022 that process heating represents about 60% of industrial energy use in American manufacturing.
Therefore, buyers should compare energy per tonne, tap-to-tap time, and standby losses. Induction may reduce onsite emissions, but grid carbon intensity determines total emissions. Gas reverberatory furnaces remain practical for high capacity, though exhaust losses need measurement.
Emissions control separates a competent installation from an impressive specification. The European Union’s Non-Ferrous Metals BREF recommends enclosed charging, extraction, filtration, and disciplined operation.
Rotary systems need strong dust and fume capture near charging points. Induction avoids combustion gases, yet fluxes and contaminated scrap still create particulates.
Controls should record temperature, power, pressure, oxygen, and filter performance.
Real plants are messier. I would not trust efficiency claims without a measured production trial.
